Chapter 1: Calibration and Debugging – Welding Torch Calibration

Chapter 1: Calibration and Debugging

Welding Torch Calibration

Step - 1

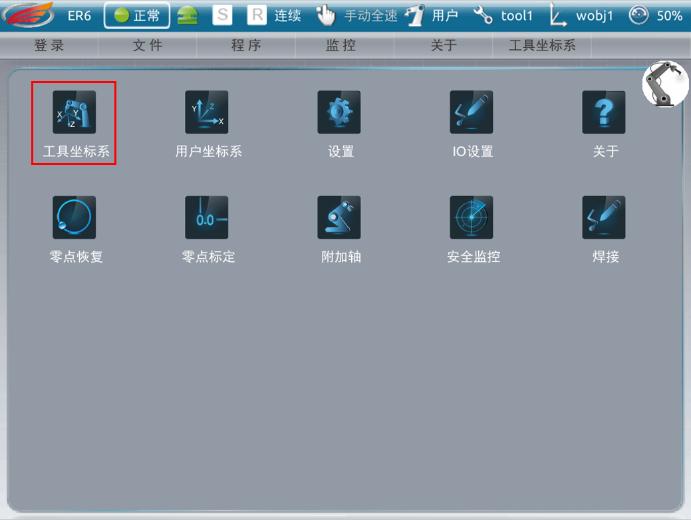
On the main interface of the teach pendant, select the Tool Coordinate System.

Step - 2

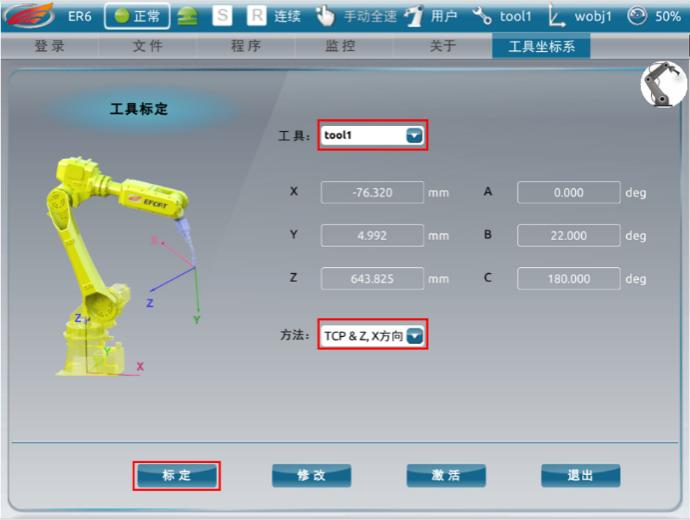
1. Select Tool: tool1 

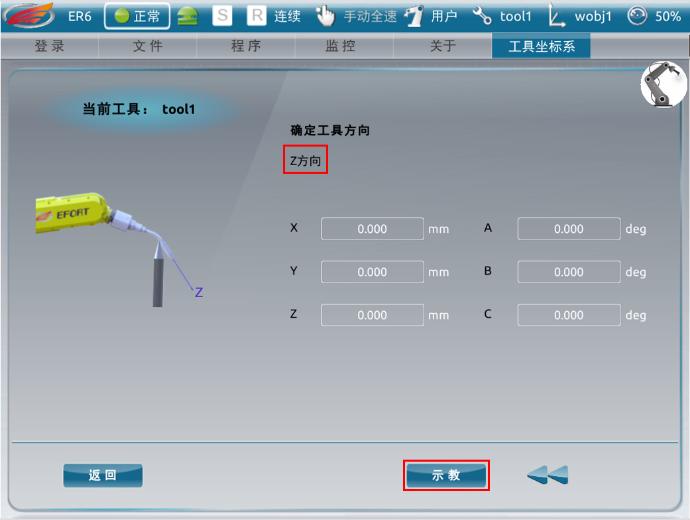
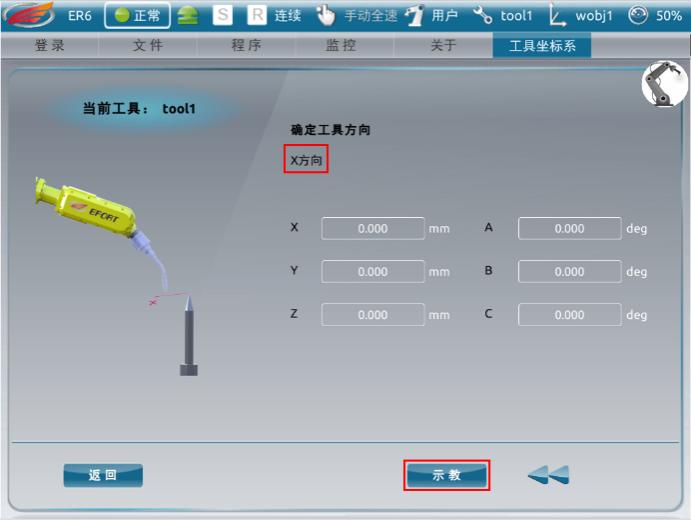
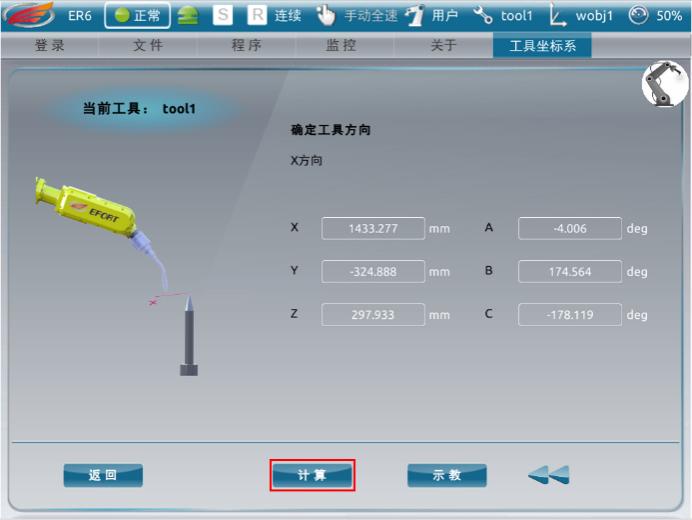
2.Select Method: TCP & Z, X Direction 

3. Click Calibrate

Step - 3

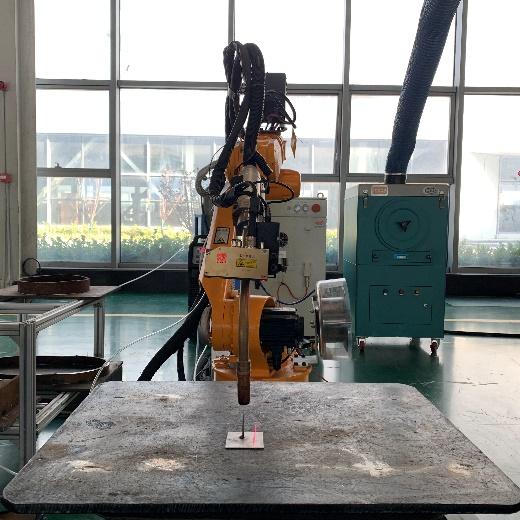
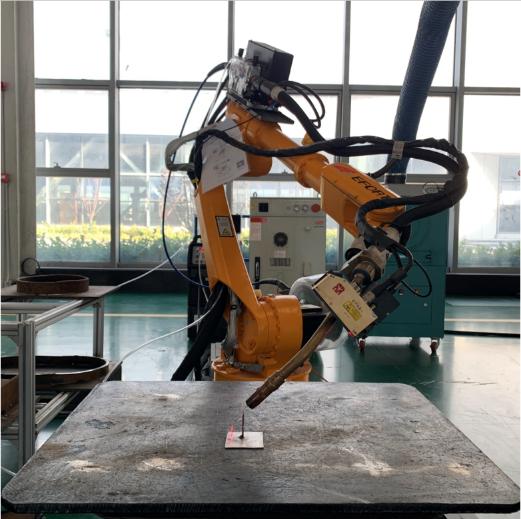
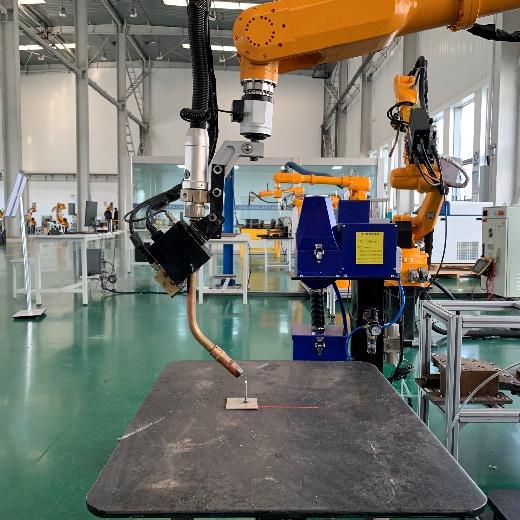
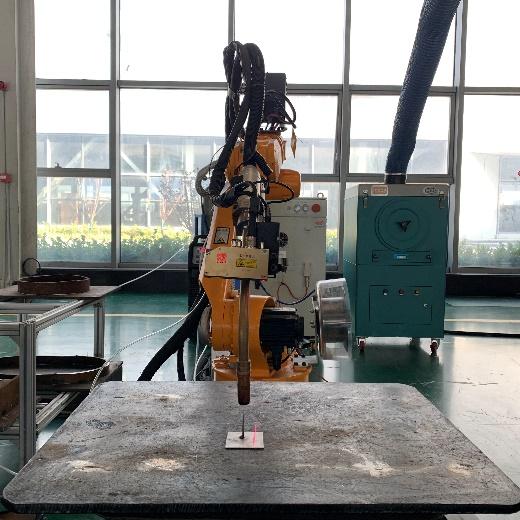
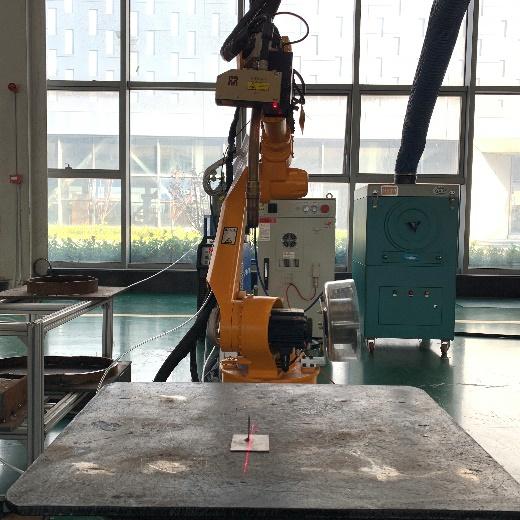
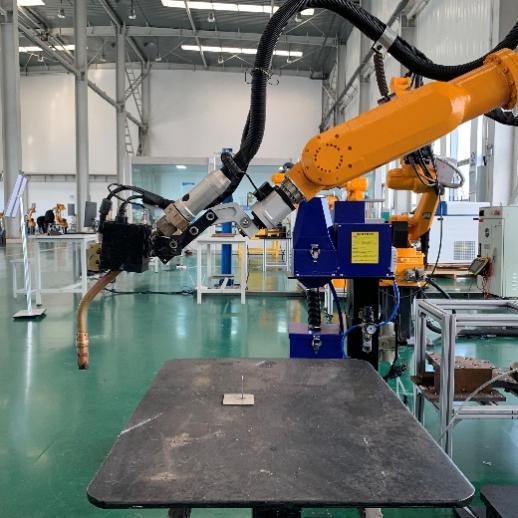
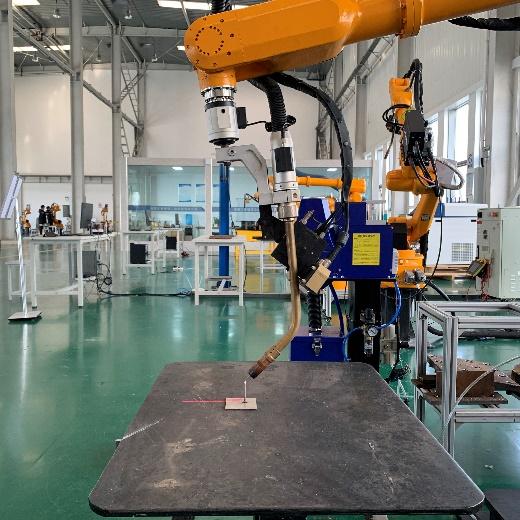
1. Adjust the welding torch to the posture of (A: 180, B: 0, C: 0), aligning it vertically with the calibration workpiece so that the welding wire just touches the tip of the workpiece.

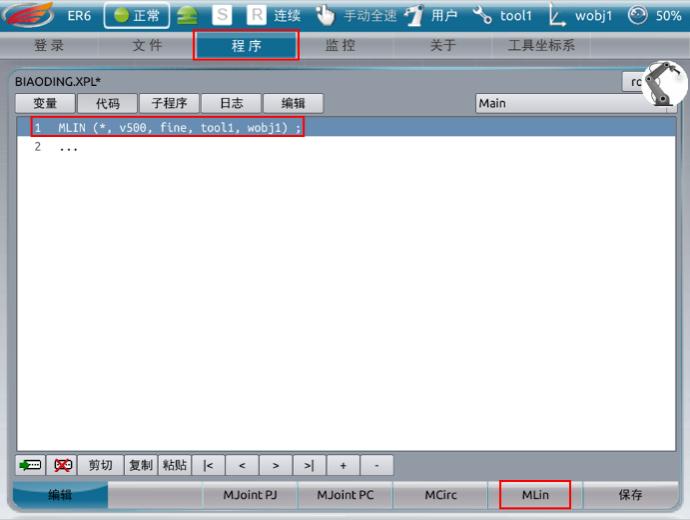
2. Use the MLin command in the program to record this point for use in the subsequent calibration of points 4 to 6.

Step - 4

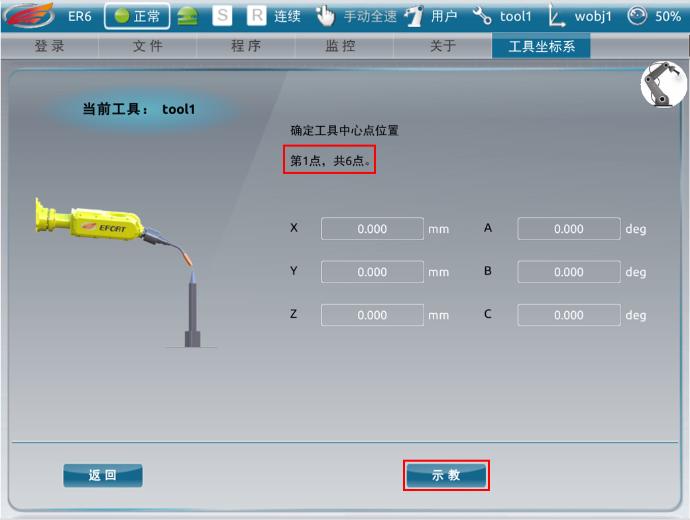
Calibrate the first point. Press the 6+ (RX) key on the teach pendant to rotate the robot counterclockwise around the X-axis. Align the welding wire with the tip of the calibration workpiece, then click Teach.

Step - 5

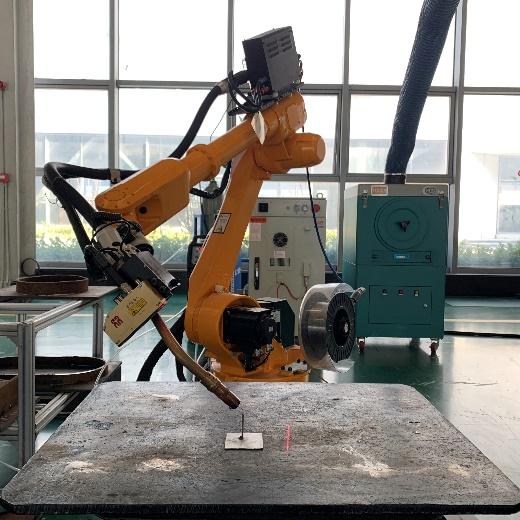
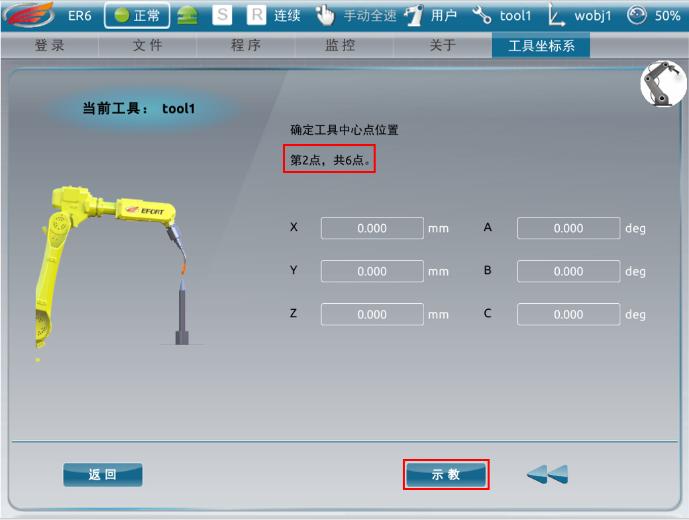
Calibrate the second point. Press the 6− (RX) key on the teach pendant to rotate the robot clockwise around the X-axis. Align the welding wire with the tip of the calibration workpiece, then click Teach.

Step - 6

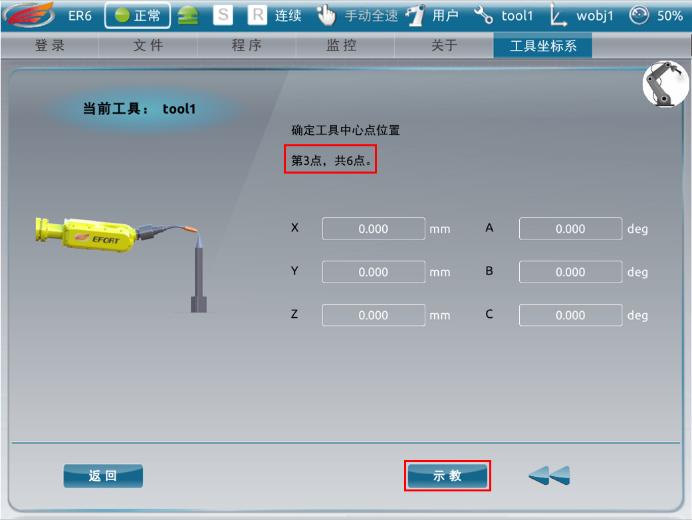
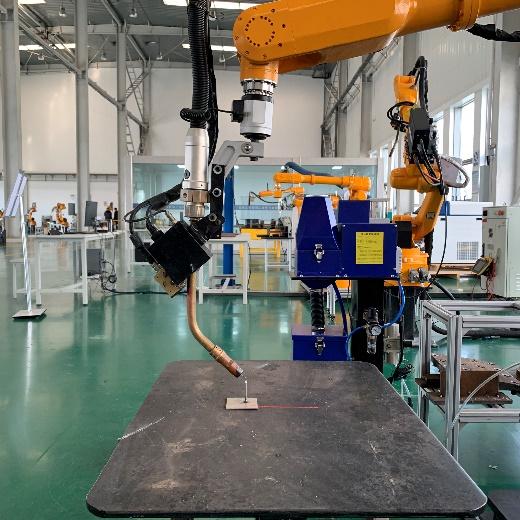
Calibrate the third point. Press the 5+ (RY) key on the teach pendant to rotate the robot approximately 45 degrees counterclockwise around the Y-axis. Align the welding wire with the tip of the calibration workpiece, then click Teach.

Step - 7

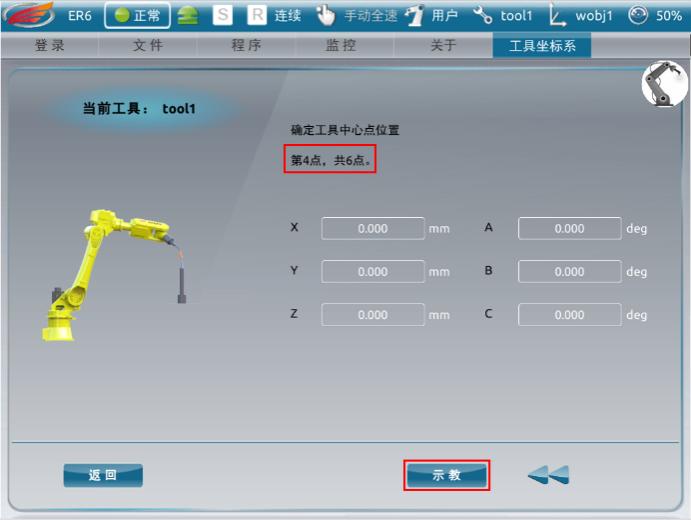
Calibrate the fourth point. Run the previously recorded program so that the TCP aligns vertically with the calibration workpiece, and the welding wire just touches the tip of the workpiece. Then click Teach.

Step - 8

Calibrate the fifth point. Run the program to return to the vertical posture. From the fourth point position, press the 3+ key to move in the positive Z-axis direction by more than 200 mm, then click Teach.

Step - 9

Calibrate the sixth point. Run the program to return to the vertical posture. From the fourth point position, press the 1− key to move in the negative X-axis direction by more than 200 mm, then click Teach.

Step - 10

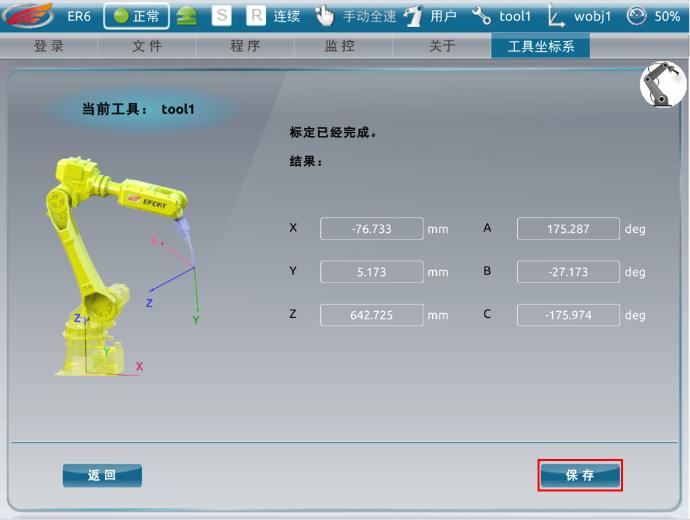
After completing the calibration, click Calculate and then Save.

Welding Torch Calibration Verification Method

Step - 1

After calibration is complete, activate Tool 1, adjust the welding torch to the posture of (A: 180, B: 0, C: 0), and align it vertically with the calibration workpiece so that the welding wire just touches the tip of the workpiece.

Step - 2

1. Press the 5+ key on the teach pendant to rotate the welding torch 45 degrees around the Y-axis. You can view the real-time torch angle in Monitor > Position. Observe whether there is any deviation during rotation.

2. If there is deviation in the Z-axis direction, adjust the X value; if there is deviation in the X-axis direction, adjust the Z value. The values can be checked in Monitor > Position.

(Note: When modifying the values, return the welding torch to the original position. The torch tip must align with the needle tip. Adjust until the torch tip stays aligned with the needle tip while rotating around the Y-axis. Ensure the deviation is within 1 mm. You may repeat the correction multiple times.)

Step - 3

1.  Adjust the welding torch to the posture of (A: 180, B: -45, C: 0) — the welding posture.

2. Press the 4+ key on the teach pendant and observe whether there is any deviation during rotation around the Z-axis.
If there is deviation in the Y-axis direction, adjust the Y value in Tool 1.
Continue adjusting until the welding torch rotates 360 degrees around the Z-axis and the torch tip remains aligned with the tip of the workpiece within a 1 mm margin of error. Once this is achieved, the correction is complete.

Comments Box SVG iconsUsed for the like, share, comment, and reaction icons
Cover for JTC Laser
JTC Laser

JTC Laser

955 Likes

Intelligent robot workstations, intelligent work islands, providing the entire process (cutting, assembly, welding, grinding, inspection, etc.) of intelligent applications for the non-standard metal structure manufacturing industry.
Classic examples of intermittent welding See MoreSee Less

1 day ago
Why use intermittent welds instead of welding the entire joint? 

More welding isn’t always better. When the design allows it, intermittent welding—also called stitch welding—offers several advantages:

✅ Less distortion: Lower total heat input helps control deformation in thin plates and long components.
✅ Higher productivity: Shorter weld lengths mean less welding time.
✅ Lower costs: Reduced consumption of welding wire, shielding gas, and electricity.
✅ Less overwelding: Provides the required connection strength for suitable stiffeners and brackets without unnecessary welding.

⚠️but Intermittent welding isn’t suitable for every application. Sealing requirements, fatigue loading, and corrosive environments require careful design consideration. Weld length, spacing, and size must follow the engineering specifications.

Where do you use intermittent welding in your production? Share your experience below!

#IntermittentWelding #StitchWelding #WeldingTechnology #SteelFabrication #RoboticWelding #ManufacturingImage attachmentImage attachment+1Image attachment

Why use intermittent welds instead of welding the entire joint?

More welding isn’t always better. When the design allows it, intermittent welding—also called stitch welding—offers several advantages:

✅ Less distortion: Lower total heat input helps control deformation in thin plates and long components.
✅ Higher productivity: Shorter weld lengths mean less welding time.
✅ Lower costs: Reduced consumption of welding wire, shielding gas, and electricity.
✅ Less overwelding: Provides the required connection strength for suitable stiffeners and brackets without unnecessary welding.

⚠️but Intermittent welding isn’t suitable for every application. Sealing requirements, fatigue loading, and corrosive environments require careful design consideration. Weld length, spacing, and size must follow the engineering specifications.

Where do you use intermittent welding in your production? Share your experience below!

#IntermittentWelding #StitchWelding #WeldingTechnology #SteelFabrication #RoboticWelding #Manufacturing
See MoreSee Less

2 days ago

It's hard to imagine how difficult it would be for a human to weld such a deep box, but a robot can weld 24/7, day and night, non-stop, and its welding quality is more consistent than that of a human. See MoreSee Less

4 days ago

Thick Plate Welding Strength Test of the 5-in-1 Welding Function See MoreSee Less

5 days ago
Load more

Latest News

Contact Details

Subscribe Us

Join our newsletter; you will receive our newest videos/tips of our laser marking, cutting, welding, cleaning and cladding machine’s latest prices and the latest promotional news


You will also get our monthly report of best products, and also coupons.

Inquire Now

Feel free to inquire now. We are always here to help you.

¡Consulta ahora!

Siéntase libre de hacer su consulta ahora. Siempre estamos aquí para ayudarlo.

استفسر الآن

لا تتردد في الاستفسار الآن. نحن دائمًا هنا لمساعدتك.

Связаться сейчас

Не стесняйтесь задавать вопросы. Мы всегда готовы помочь вам.